Business Details
35 Years
experience
Your Trusted Partner for Industrial Lighting Solutions
Established in 1991, Victory Lighting has grown from a UK-based manufacturer into a global leader in infrared and ultraviolet lighting technology. Our expertise spans industrial, commercial, and specialised applications, with a focus on precision heating, disinfection, and curing systems. As a Made in Britain member, we combine British engineering excellence with global distribution networks, operating across Europe, North America, and Asia. Our dedicated R&D facility in Leighton Buzzard drives continuous innovation, while our commitment to sustainability shapes energy-efficient solutions and responsible manufacturing practices. With decades of technical expertise, we partner closely with clients to optimise manufacturing processes through tailored IR and UV systems.Our team of specialists, including seasoned engineers and industry professionals, ensures every project benefits from in-depth knowledge and practical experience. Through strategic acquisitions like DPL Industri, we've expanded UK manufacturing capabilities to deliver faster lead times and greater customisation. Trusted by sectors ranging from healthcare to aerospace, our products undergo rigorous TV SD testing to guarantee compliance with international standards. This combination of technical excellence, ethical practices, and customer-centric solutions has cemented our position as a market leader in lighting technology.
Services
Infrared Lamps
Ultraviolet Lamps
Custom Solutions
Paint Dryers
Germicidal Lamps
Details
- Year established: 1991
Highlights and features
- 34 years of specialist expertise in IR and UV lighting technology since 1991
- UK-based manufacturing with ISO-standard quality control processes
- Dedicated R&D facility driving continuous product innovation
- Global distribution network covering 5 continents
- Sustainability-focused solutions with mercury-free UV technology
Associations and certifications
- Made in Britain
- TV SD
What people say
Exceptional product quality
Outstanding service
Reliable solutions
Technical expertise
Long-term partnership
Services
Infrared Lamps
Our infrared lamps deliver precision heating for industrial applications, featuring durable construction and energy-efficient performance. Designed for sectors like automotive and food processing, these UK-manufactured lamps ensure consistent thermal output. Backed by 34 years of technical expertise, our solutions optimise production processes while meeting international safety standards through TV SD certification.
Ultraviolet Lamps
Specialist UV lamps provide disinfection and curing solutions across healthcare and manufacturing sectors. Our mercury-free technology reduces environmental impact while maintaining effectiveness. Custom configurations meet specific industry requirements, supported by comprehensive technical documentation and global distribution infrastructure spanning five continents.
Custom Solutions
Tailored IR and UV systems address unique operational requirements, from concept through to delivery. Our engineering team develops application-specific solutions, leveraging in-house R&D capabilities and UK manufacturing facilities. This approach ensures optimal performance in challenging environments while maintaining compliance with international standards.
Paint Dryers
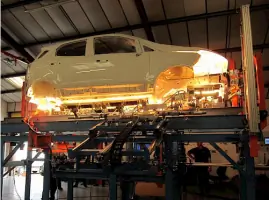
Infrared paint drying systems accelerate finishing processes without compromising quality. Engineered for industrial applications, these systems improve throughput while reducing energy consumption. Backed by technical support from our experienced team, the solutions integrate seamlessly into existing production lines.
Germicidal Lamps
UV-C germicidal lamps effectively neutralise microorganisms in water and air treatment systems. Designed for healthcare and food processing applications, these lamps combine proven technology with modern efficiency improvements. The solutions benefit from our Made in Britain manufacturing standards and global technical support network.
People
Alan Penman
Group Chairman
With over three decades of leadership, Alan has guided Victory Lighting's transformation from a small UK manufacturer to a global enterprise. His strategic vision established international operations across three continents while maintaining core British manufacturing values.
Tyler Penman
Managing Director
Driving operational excellence, Tyler oversees global strategy implementation and business development. His expertise in lighting technology has expanded the company's market presence through targeted acquisitions and innovation in sustainable solutions.
Toby
Sales Director
Leading sales operations, Toby has strengthened international partnerships and distribution networks. With technical knowledge spanning two decades, he ensures client requirements translate into effective lighting solutions for diverse industrial applications.
Charles Ramsdale
Technical Manager
Managing technical operations, Charles oversees product development and quality assurance. His engineering expertise ensures solutions meet rigorous international standards while driving innovation in energy-efficient lighting technologies.
Bart Licki
Quality Assurance Manager
Bart implements quality control systems that maintain Made in Britain standards across global production facilities. His work ensures compliance with TV SD testing requirements and continuous improvement in manufacturing processes.
Questions
What industries do your lighting solutions serve?
Our IR and UV solutions serve automotive, healthcare, food processing, aerospace, and manufacturing sectors with tailored applications.
Are your products manufactured in the UK?
Yes, we maintain UK manufacturing facilities as part of our Made in Britain commitment, with additional operations in Europe and Asia.
How do you support international customers?
Through regional offices in Europe and North America, plus a global distribution network covering five continents with localised support.
What sustainability initiatives do you have?
We use biodegradable packaging, operate energy-efficient facilities, and develop mercury-free UV technology to reduce environmental impact.
Can you provide custom lighting solutions?
Our engineering team designs bespoke IR and UV systems tailored to specific industrial requirements, from concept to delivery.
Videos